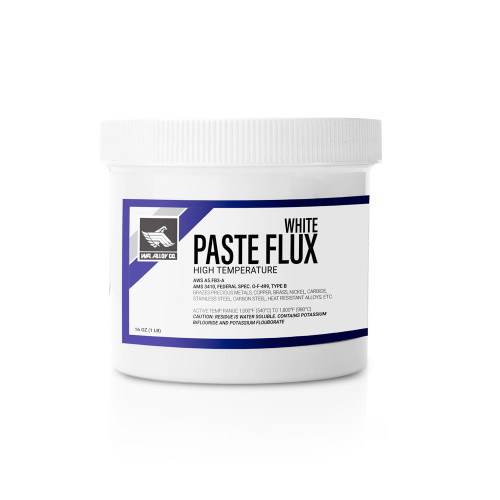


SUPERFLOW White Brazing Paste Flux – 1 lb Container
General-purpose white brazing flux for silver and phos-copper brazing alloys.
SUPERFLOW White Brazing Paste Flux is an AWS A5.31 FB3-A general-purpose brazing flux designed for use with silver brazing alloys and phos-copper alloys. Its smooth, creamy consistency makes it easy to apply to prepared joints before brazing.
The flux is commonly used when joining compatible combinations of copper, brass, steel, bronze, and certain stainless steels. It is formulated to resist hardening and crystallization, helping it retain its smooth, creamy texture for a minimum of one year under proper storage conditions.
Package Size: Supplied in a 1 lb (16 oz) container.
Key Features
- General-Purpose Brazing Flux: Designed for a wide range of professional brazing applications.
- Silver Brazing Alloys: Suitable for use with compatible silver brazing filler metals.
- Phos-Copper Alloys: Can also be used with compatible phos-copper brazing alloys.
- AWS FB3-A: Classified to AWS A5.31 FB3-A.
- Wide Active Temperature Range: Active from 1050–1600°F (565–870°C).
- Creamy Paste: Smooth consistency makes the flux easy to apply to prepared joints.
- Water-Soluble Residue: Residue can be cleaned with hot water after the brazed assembly has cooled.
- Multiple Base Metals: Commonly used with compatible copper, brass, steel, bronze, and certain stainless steels.
- Stable Consistency: Formulated to resist hardening and crystallization and retain its creamy texture for a minimum of one year.
- 1 lb Container: Supplied in a 16 oz package.
Compatible Brazing Applications
SUPERFLOW White Brazing Paste Flux is commonly used when brazing compatible combinations of:
- Copper
- Brass
- Steel
- Bronze
- Certain stainless steels
- Compatible dissimilar-metal joints
- Silver brazing alloy applications
- Phos-copper brazing alloy applications requiring flux
Physical Data
| Active Temperature Range | 1050–1600°F (565–870°C) |
|---|---|
| Form & Color | White Creamy Paste |
| Water Content | Less Than 35% |
| pH | 8.0–8.5 |
| Specific Gravity | 1.6 |
| Flash Point | None |
| Effects of Freezing | None |
| Residues | Water-Soluble |
How to Use SUPERFLOW White Brazing Flux
SUPERFLOW White Brazing Paste Flux may be used directly from the container. If a thinner consistency is needed, Washington Alloy states that water may be added.
For best results, heat the flux indirectly by bringing the base metal up to the required brazing temperature rather than concentrating the flame directly on the flux.
After the brazed assembly has cooled, Washington Alloy recommends cleaning the remaining flux residue with hot water at approximately 140°F (60°C).
Why Use Brazing Flux?
Brazing flux helps prepare and protect the joint area during heating so compatible brazing filler metal can properly wet and flow across the prepared base-metal surfaces.
SUPERFLOW White Brazing Flux is particularly useful with silver brazing alloys and in applications where the selected filler metal or base-metal combination requires flux during the brazing process.
Package Information
| Package Type | Plastic Container / Jar |
|---|---|
| Net Weight | 1 lb |
| Net Contents | 16 oz |
Note: Product packaging and label appearance may vary.
Frequently Asked Questions
What is SUPERFLOW White Brazing Flux used for?
It is a general-purpose brazing paste flux designed for use with compatible silver brazing alloys and phos-copper brazing alloys.
What is the AWS classification?
SUPERFLOW White Brazing Flux is classified as AWS A5.31 FB3-A.
What metals can it be used with?
Washington Alloy identifies copper, brass, steel, bronze, and certain stainless steels among its common applications.
What temperature range is the flux active in?
The active temperature range is 1050–1600°F (565–870°C).
How much flux is included?
This listing includes one 1 lb (16 oz) container of SUPERFLOW White Brazing Paste Flux.
Can the flux be thinned?
Yes. Washington Alloy states that water may be added when a thinner consistency is needed.
How should I heat the flux?
For best results, Washington Alloy recommends heating the flux indirectly by bringing the base metal to the required temperature.
How do I clean the flux residue?
Allow the brazed assembly to cool, then clean the water-soluble residue using hot water at approximately 140°F (60°C).
Will the flux harden during storage?
Washington Alloy states that the product is formulated not to harden or crystallize and to retain its smooth, creamy texture for a minimum of one year.
-
Welding Process
Brazing -
Form
Paste -
Color
White -
Active Temperature Range
1050–1600°F (565–870°C) -
Residue
Water-Soluble

SUPERFLOW Black Brazing Paste Flux
Starting at
$22.99

SUPERFLOW 45 CF, High-Silver Brazing Alloy (BAg-5)
Starting at
$113.99
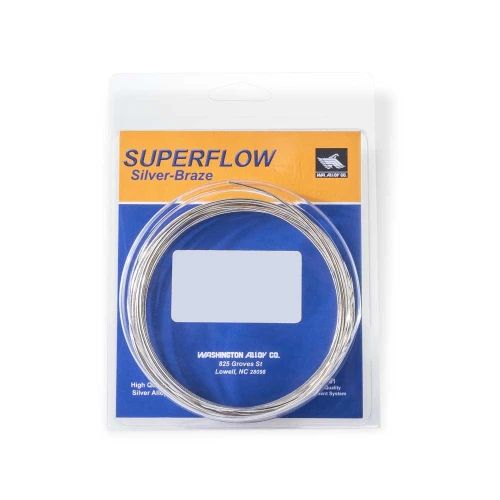
SUPERFLOW 56 CF, Cadmium-Free Silver Brazing Alloy (BAg-7)
Starting at
$138.99
Have a question? Ask our team
 (0) Reviews
There are no reviews associated with this product.
Write a Review